Three-Phase Current Transformer Company Selection Factors Every Engineer Should Review
2026-10-21
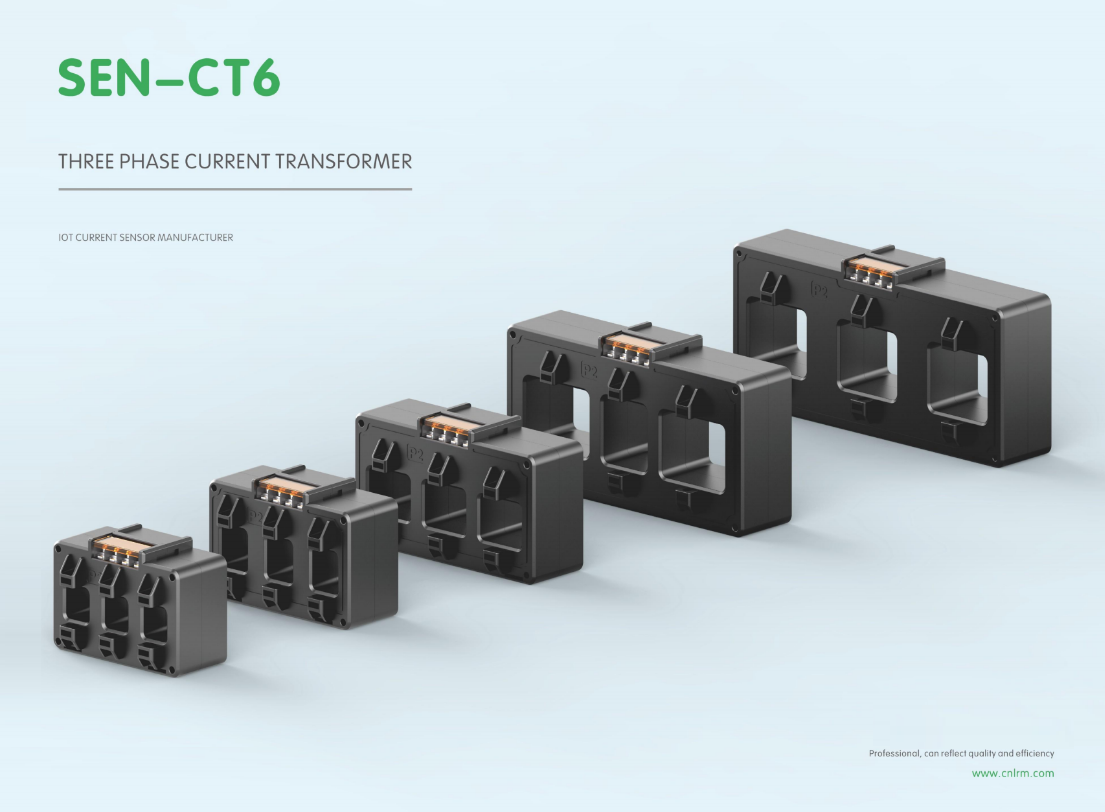
Every engineer knows that three-phase current transformers are critical, but not every engineer questions the company behind the nameplate. A supplier's testing rigor, insulation materials, and support response can make or break your project. This guide breaks down the selection factors that matter most—and why Xiasen consistently clears the bar in demanding applications.
Datasheet accuracy claims worth challenging before you commit
Datasheets often read like polished resumes—every spec dressed up, every performance figure cherry-picked from a lab bench that barely resembles your real circuit. Before you trust those headline numbers, take a close look at how they were measured. For instance, a regulator might claim 95% efficiency, but that could be at a single sweet-spot load with ideal input voltage and a perfectly laid-out evaluation board. Swap in your own inductor, add a few centimeters of trace, and run it at half load—suddenly you’re staring at 82%. The datasheet isn’t lying; it’s just not telling you the whole story. Dig into the test conditions, the component tolerances, and the thermal assumptions. If the fine print is missing or vague, treat that spec as a starting point, not a promise.
Another common trap is the “typical” value printed in bold while the min/max columns stay blank or show absurdly wide spreads. A comparator might list 5 mV offset as typical, but without a guaranteed maximum, you could be designing for a lottery. Ask yourself: what happens to my circuit if every “typical” drifts to its worst-case extreme? Run the math with the full temperature range, supply variation, and aging effects. If the vendor can’t provide distribution data or characterization over -40°C to +125°C, you’re essentially beta-testing their silicon. That might be fine for a hobby project, but for anything that ships in volume or goes into the field, you need more than a hopeful average.
Finally, challenge the dynamic specs—the ones that look great in steady state but fall apart under real signal conditions. An ADC’s signal-to-noise ratio might be measured with a full-scale sine wave at one exact frequency, while your signal is a bursty, low-level pulse train. A MOSFET’s switching loss could be quoted with zero gate resistance and ideal snubbers, but your layout adds 5 nH of stray inductance. Ask for load-step responses, PSRR curves across frequency, and EMC behavior with real board parasitics. If the datasheet only shows one pretty waveform at room temperature, it’s time to request an evaluation board and run your own tests—because committing to a part based on marketing-grade accuracy claims is how you end up with a product that works on paper and nowhere else.
Why insulation coordination decides more than the spec sheet suggests
A spec sheet lists rated voltages, BIL, and creepage distances as if they were fixed thresholds. But once a substation or line is energized, the actual stresses deviate quickly: switching surges, resonance with cable capacitance, and lightning-induced transients all arrive with faster rise times and higher peaks than standard tests suggest. Insulation coordination becomes the real arbiter of whether a “compliant” design survives its first storm season—or quietly degrades insulation until a routine switching operation turns into a flashover.
Altitude, pollution, and humidity rarely match the clean, standardized lab conditions behind catalog data. A 20% derating at 2,000 meters sounds manageable on paper, yet combined with wet salt deposits on bushings and uneven voltage distribution across a string of insulators, it can push local electric fields beyond critical limits. The spec sheet assumes uniform stress, but the field never is; coordination studies expose where weak points will actually form.
Good coordination also ties the insulation level to the protection system, not just to a nameplate number. If the surge arrester’s energy rating is marginal, its residual voltage may climb above the equipment’s chopped-wave withstand, leaving the transformer exposed despite passing all factory tests. Matching the protective margins, grounding scheme, and expected overvoltage durations often dictates a different insulation class than what a simple spec comparison would recommend—and that gap is where unexpected outages are born.
Fault current survival: the thermal rating nobody checks until it's too late
Most design reviews obsess over the instantaneous peak of a short circuit—will the busbars bend, will the breaker interrupt? But the real killer often arrives quietly, in the seconds after the fault begins. Thermal ratings sit buried in datasheets, rarely cross-checked against actual protection clearing times. Then one day a transformer smells like burnt varnish, or a switchgear contact welds itself shut, and everyone suddenly remembers that heat doesn't care about your fault study's pretty graphs.
The math is simple enough: I²t. Current squared, times time. Not peak current, but the relentless accumulation of resistive heating during every cycle the fault persists. A modest fault current flowing for two seconds can cook insulation far worse than a massive spike cleared in three cycles. Yet field settings for relays often drift upward over the years, coordination studies get stale, and nobody rechecks whether the cable can actually survive the new trip curve. By the time the thermal damage shows up, the equipment is already a write-off.
Fitting three-phase CTs into switchgear without a mechanical headache
Getting three current transformers into an existing switchgear panel often feels like trying to park a bus in a bicycle shed. The CTs themselves are bulky, the busbars don't leave much room, and the mounting brackets rarely line up with what's already there. Most mechanical headaches come from trying to force a standard CT footprint into a space that was never designed for it.
A smarter approach is to treat the CT installation as a layout problem rather than a component problem. Look for split-core or low-profile CTs that can slip around existing conductors without dismantling the whole busbar assembly. If the panel has any spare DIN rail or side wall space, use adjustable mounting plates that let you shift the CTs a few millimeters in any direction. Pre-drilling templates help, but the real trick is to dry-fit everything outside the panel first, then transfer the layout inside.
When the mechanical fit is right, the electrical performance follows. CTs that are wedged in or resting against busbar insulation tend to vibrate, loosen, or develop hot spots over time. Take the extra hour to secure them with proper standoffs and torque the mounting hardware to spec. It removes the future maintenance callbacks and keeps the switchgear looking like someone actually planned the installation.
The real cost of calibration, lead times, and post-installation support
Calibration rarely shows up on the purchase order, but it should. Depending on the instrument, a single certified calibration can run anywhere from a few hundred to several thousand dollars, and that’s assuming nothing drifts out of tolerance. If your process demands traceability to NIST or ISO 17025, expect recurring fees, shipping costs, and days of downtime while the unit is out for service. The real sting comes when a sensor fails calibration mid-cycle—suddenly you’re paying for an emergency turnaround, expedited shipping, and possibly re-validation of your entire measurement chain.
Lead times are another budget line that gets ignored until it’s too late. Off-the-shelf components might ship in a week, but customized ranges, exotic fittings, or firmware tweaks can push delivery to twelve or sixteen weeks. That gap forces you to either stock spares you didn’t plan for or risk halting a production line. And if the supplier’s own suppliers are backed up—common for pressure cells, specialty alloys, or precision electronics—the date on the quote can slip without warning, turning a two-month project into a five-month one.
Post-installation support is where the total cost of ownership quietly climbs. The base warranty often covers defects but not wear, environmental damage, or user error. When a transmitter fails at 2 a.m., a same-day service call might cost more than the device itself once travel, labor, and emergency fees are added. Then there’s the soft cost of training maintenance staff, keeping calibration records audit-ready, and maintaining a spare parts inventory. None of this appears in the upfront quote, yet over a five-year lifecycle it can easily double or triple the original purchase price.
Reading test reports: separating lab results from your actual operating conditions
Lab reports look authoritative, but the numbers come from tightly controlled benches. Your equipment in the field deals with fluctuating temperatures, unstable voltage, and often a completely different fluid or gas. Treating those lab figures as if they were real-world performance guarantees usually leads to disappointment.
Before you jump to conclusions, check what fluid was used, what load cycle was applied, and what ambient temperature was set. In actual operation you may never run the machine in that ideal steady state. Frequent starts and stops, partial loads, dust, and humidity all shift behavior away from the published curves.
A practical approach is to treat the test report as a baseline, not a promise. Find the test points closest to your site conditions, then correct for the differences or run your own spot checks. If the lab used clean water and you are pumping a high-viscosity or particle-laden liquid, expect efficiency, wear, and even noise to move off the table values.
FAQ
Start with the company's track record in your specific industry. Ask for reference installations that match your voltage and current ranges, and don't hesitate to contact those customers directly. A supplier with proven performance under similar load conditions will save you from surprises later.
Accuracy class is not just a datasheet number—it determines whether your metering or protection scheme will function correctly. Look for a manufacturer that can provide test reports and temperature stability curves, not just a claimed class. Split-core and solid-core options may differ in long-term drift.
Yes, consider lead time, custom tap configurations, and the cost of re-certification if you need to modify specs later. Some companies charge extra for burden testing or field support. A slightly higher unit price from a responsive supplier often beats a cheap quote that delays commissioning.
The housing must withstand the installation environment—think humidity, chemical exposure, UV, or vibration. A supplier that offers polycarbonate, epoxy, or metal enclosures and can explain the trade-offs shows real engineering depth. Cheap housings crack or degrade, leading to early failures.
A serious CT manufacturer will have in-house routine tests for ratio, polarity, excitation, and insulation resistance, plus type tests for short-time thermal current. Ask to see their calibration certificates and whether they follow IEC or IEEE standards. Without independent verification, you're trusting marketing claims.
Request a sample and see how they handle questions about installation orientation, lead connection, or burden mismatch. A company that assigns an application engineer rather than a sales rep can help you avoid misapplication. Check if they provide clear mounting diagrams and derating guidance.
Not always, but flexibility matters when you have non-standard busbar sizes or tight enclosures. A supplier willing to adjust window dimensions, add electrostatic shielding, or provide multi-ratio taps can save redesign costs. Just confirm they don't charge a premium for minor modifications.
Look beyond CE marking. For North America, UL 2808 or IEEE C57.13 compliance indicates robust design. For global projects, IEC 61869 series is key. Also verify ISO 9001 quality management—it's a baseline, not a differentiator, but its absence is a red flag.
Conclusion
Selecting a three-phase current transformer supplier requires digging past glossy datasheet claims. Accuracy figures often assume idealized burden and frequency conditions that vanish once installed in a switchgear panel with adjacent busbars and uneven load sharing. Insulation coordination is another silent determinant: a CT rated for a certain voltage class may still fail under transient overvoltages if the creepage and clearance distances don't match your actual pollution degree and altitude. Fault current survival is equally unforgiving. The thermal short-time rating might look adequate on paper, but many engineers overlook the dynamic peak withstand current or the secondary winding's thermal limit during a close-in fault. These aren't numbers to trust without asking how they were derived and whether they reflect your protection scheme's worst-case clearing time.
Mechanical fit often becomes the last-minute crisis that delays panel assembly: busbar window dimensions, mounting foot patterns, and terminal orientation rarely match the catalog drawings once you add cable lugs and bending radii. Beyond the hardware, the real cost equation includes calibration turnaround, extended lead times for non-standard ratios, and whether the manufacturer provides field support after commissioning. Test reports deserve the same skepticism as marketing copy. A laboratory type test at 23°C with ideal grounding won't predict behavior in a humid substation with unbalanced phase currents and harmonic distortion. Ask for reports performed at your rated frequency, burden, and ambient range, and compare those conditions against your own site measurements before making a final call.
Contact Us
Contact Person: Liu Mengyang
Email: [email protected]
Tel/WhatsApp: 8618727589233
Website: https://www.cnlrm.com/en/