Single Shaft Shredder Fabrication: Key Steps and Material Considerations for Robust Builds
2026-08-02
Ever wondered what goes into building a single shaft shredder that truly lasts? From initial design to final assembly, every decision—whether it’s the alloy choice for blades or the welding technique—determines whether your machine will excel or fail under tough conditions. At Shengzhong Shredder, we’ve learned that robust fabrication isn’t just about heavy steel; it’s about precision engineering and material science working together. In this article, we’ll walk you through the critical steps and material considerations that separate a reliable workhorse from a costly mistake, so you can build or specify a shredder that meets the demands of modern waste processing.
Designing the Core: Geometry and Force Distribution
At the heart of any load-bearing structure lies its core—a central element engineered to handle complex forces efficiently. The geometry of this core is rarely accidental; it is meticulously shaped to direct compressive, tensile, and shear forces along paths that minimize stress concentrations. Whether it’s a hexagonal pattern inspired by honeycombs or a sweeping arch that echoes ancient bridges, the form itself becomes a silent calculus, distributing weight and resisting deformation through sheer spatial logic.
Force distribution within the core hinges on how well the design aligns with the primary load paths. A well-tuned core doesn’t fight the forces—it guides them, channeling energy away from vulnerable points and toward stronger, often wider, sections. Subtle adjustments, like tapering a column or adding a fillet at a sharp corner, can dramatically reduce peak stresses. This balancing act between material and void creates an internal harmony where every curve and angle serves a purpose, turning a static block into a dynamic, responsive skeleton.
Modern computational tools allow designers to iterate through countless variations, but the underlying principles remain rooted in physics. By studying how natural structures—from bamboo stalks to human femurs—handle combined loading, engineers extract timeless strategies for core design. The result is an object where geometry and force distribution are inseparable, each informing the other until the boundary between art and mechanics blurs into a single, resilient whole.
Material Selection: Balancing Wear Resistance and Cost
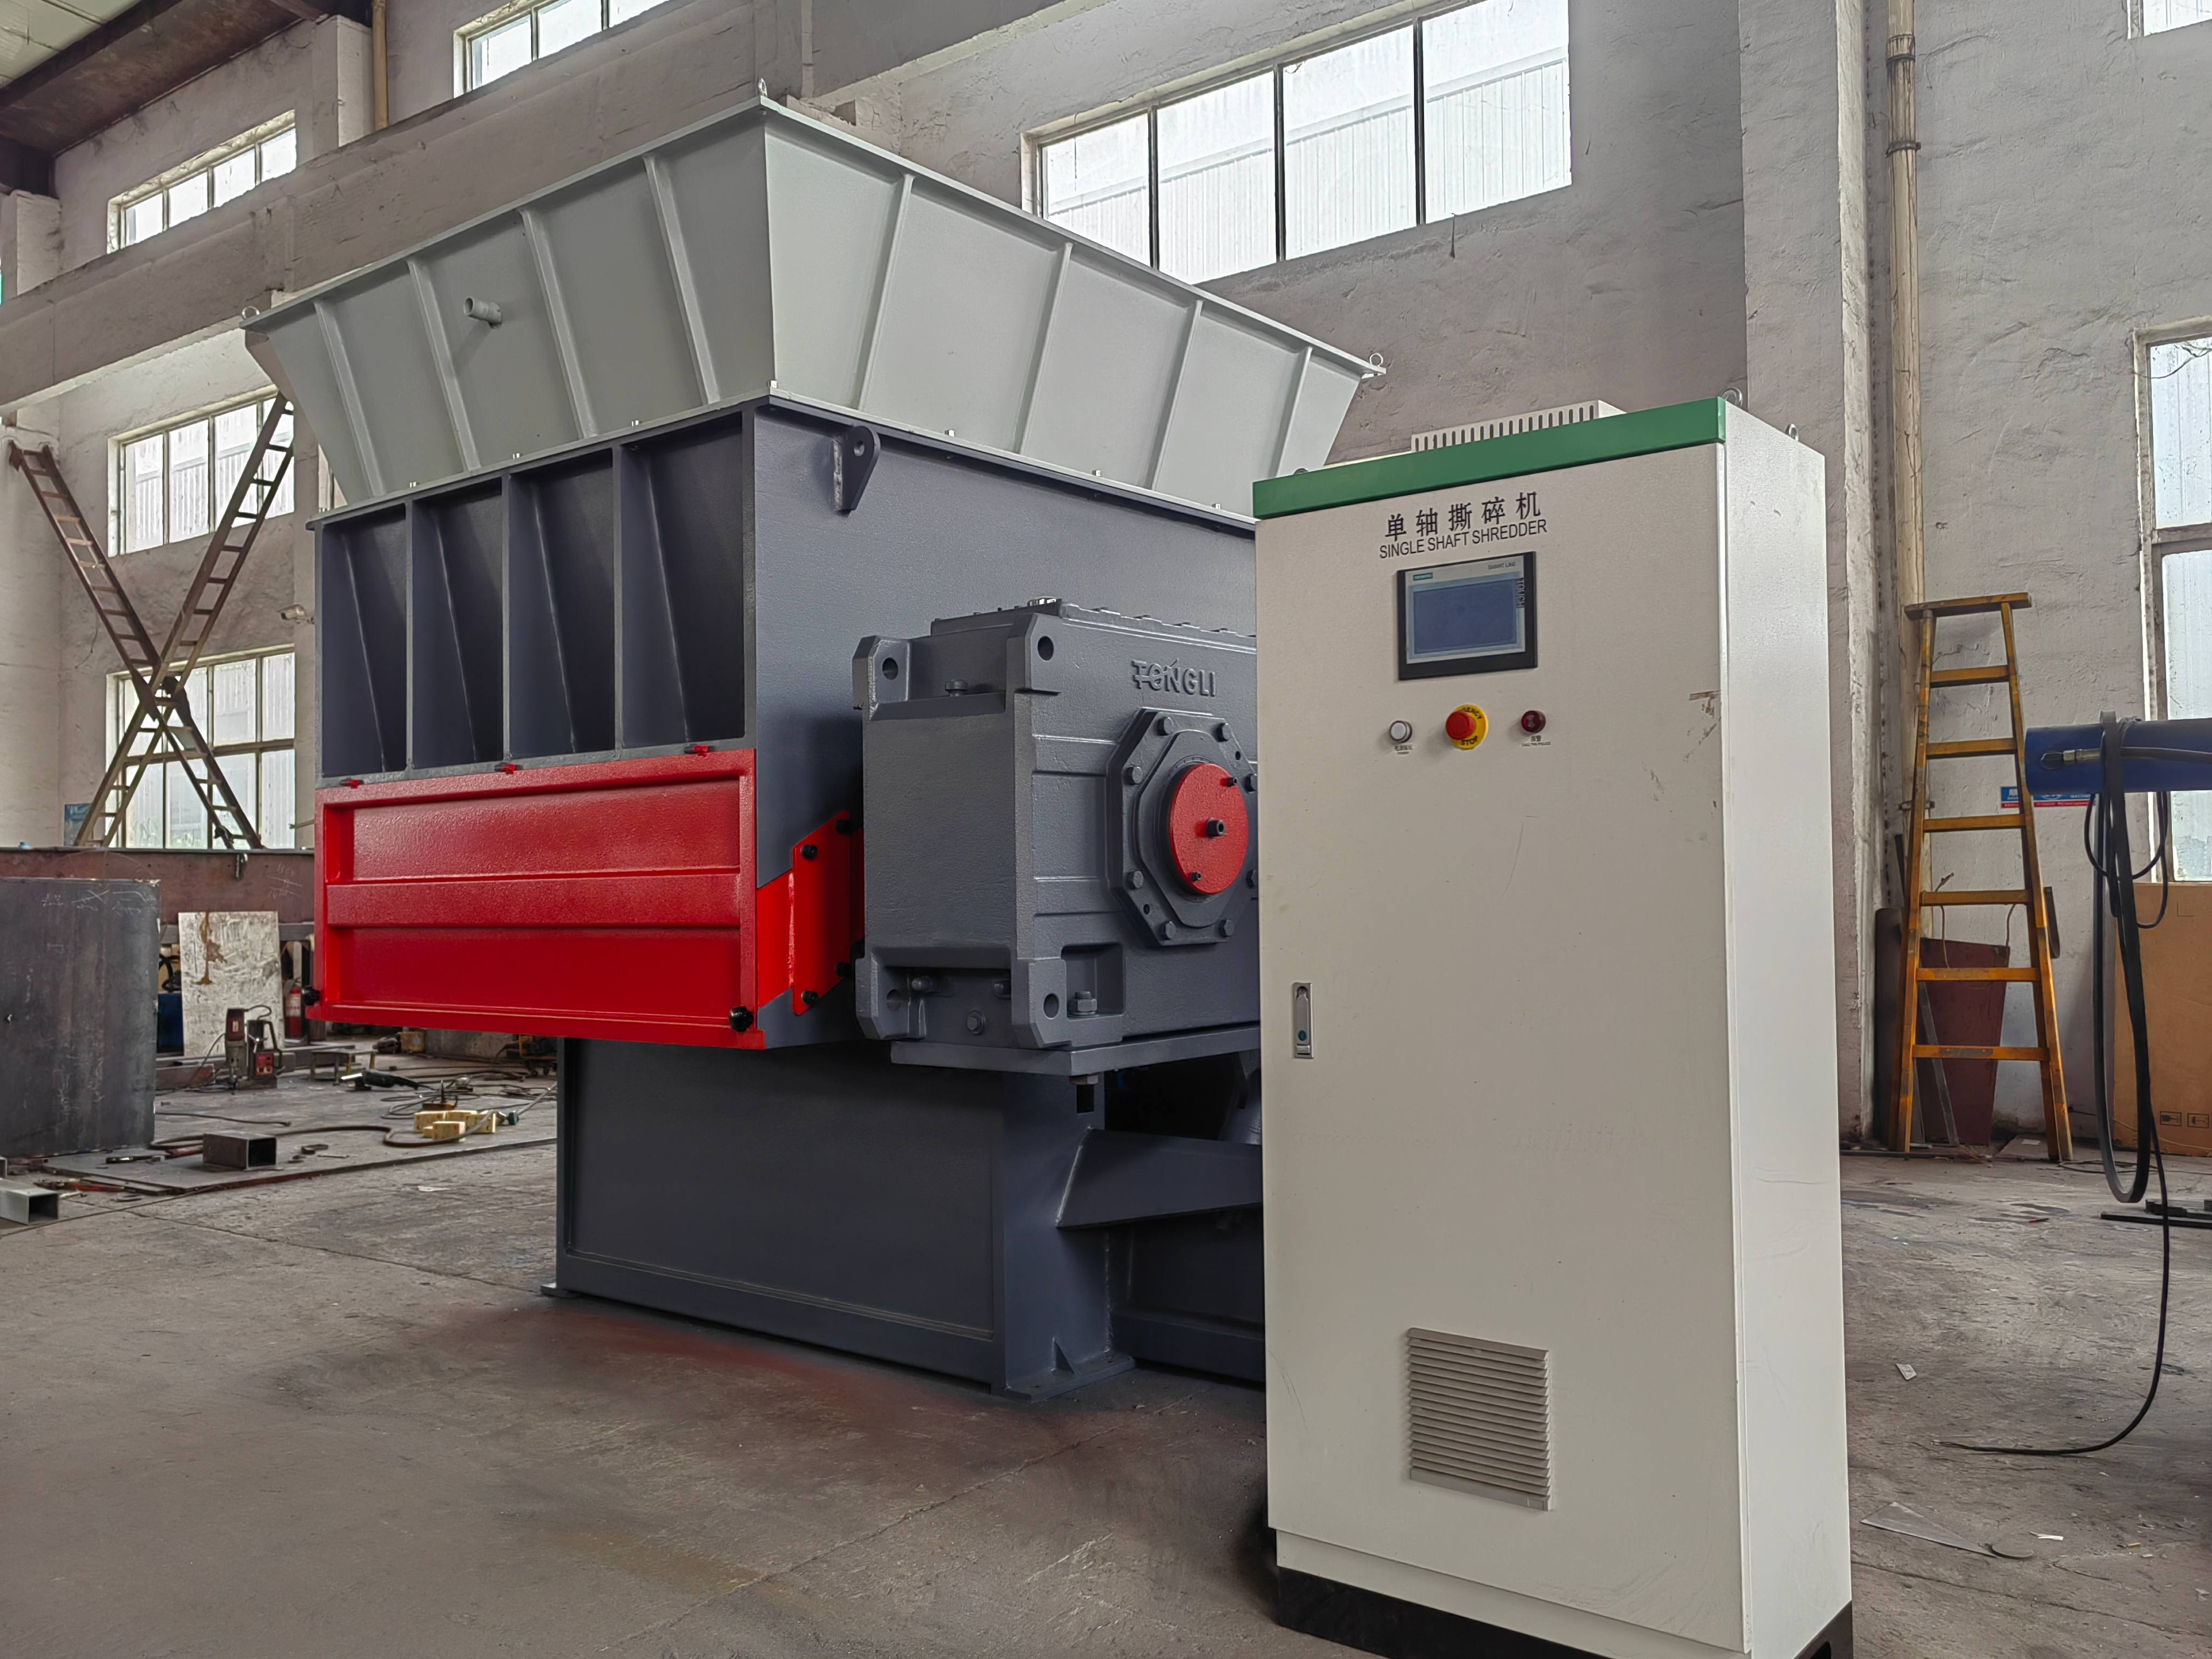
Selecting the right material is a constant tug-of-war between durability and budget. You might instinctively lean toward premium alloys or hardened steels for their exceptional wear resistance, but the cost can quickly spiral, especially for large-scale or single-use components. Conversely, opting for cheaper, softer materials may shrink upfront spending but invites frequent replacements, downtime, and potential damage to mating parts—eating into any initial savings over time.
The sweet spot often lies in engineered compromises. For instance, surface treatments like nitriding or chrome plating can transform an affordable base metal into a wear-resistant workhorse at a fraction of the cost of a fully high-spec material. Similarly, using inserts or coatings only in high-stress zones concentrates performance where it’s needed most, rather than across the entire part. This targeted approach keeps overall spend down while still guarding against abrasive, adhesive, or erosive wear.
Ultimately, the evaluation should be lifecycle-driven, not just a comparison of purchase prices. Factor in expected service life, maintenance intervals, and the consequences of failure. A slightly more expensive material that doubles the lifespan of a critical component can deliver far lower cost-per-cycle. By analyzing wear mechanisms and operating conditions specific to your application—be it sliding contact, particle impact, or corrosive wear—you can map material properties like hardness, toughness, and corrosion resistance to actual needs, avoiding both over-engineering and short-sighted economizing.
Forging the Blades: Heat Treatment and Hardness Optimization
A blade’s soul isn’t fully awakened until fire and discipline shape its final structure. Heat treatment is where steel truly answers the maker’s intent—turning what was once a soft, workable blank into a cutting tool that holds its edge under hard use. Skipping or rushing this stage leaves you with a shape that looks like a knife but behaves like a butter spreader.
The process begins with austenitizing: bringing the blade to a critical temperature where the iron lattice restructures, dissolving carbides into solution. A fast quench then locks that arrangement into a hard, brittle martensite—too fragile right out of the quench. Tempering follows, a careful reheating that trades some hardness for toughness, dialing the blade from glass-sharp fragility to a durable cutting edge. Timing and temperature control here aren’t just numbers; they’re the difference between a blade that chips on bone and one that sings through it.
Hardness optimization means pushing the steel to its practical limit for the intended job. A fillet knife can sit at 60 HRC and glide through flesh, while a chopper near 56–58 HRC withstands shock without shattering. Simple rockwell tests confirm what you feel in the hand—resistance to deformation. But true optimization comes from matching the heat recipe to the alloy, the cross-section, and the expected abuse. Nothing mass-produced nails that feel of a blade hardened just right, every molecule aligned by someone who understood fire.
Frame Fabrication: Welding Techniques for Structural Integrity
The backbone of any durable frame lies in the precision of its welded joints. Rather than relying on a single method, skilled fabricators often combine techniques—like pulsed MIG for deep penetration on thick sections and TIG for delicate, high-strength tie-ins—to create a seamless, crack-resistant structure. This hybrid approach not only ensures a uniform grain structure but also minimizes distortion, a common culprit in premature fatigue failures.
Controlling heat input is just as critical as filler metal selection. By preheating alloys prone to hardenability and carefully managing interpass temperatures, fabricators prevent the formation of brittle microstructures that compromise toughness. Post-weld treatments, such as peening or localized stress relief, further lock in dimensional stability, ensuring the frame can withstand cyclic loading without gradual deformation.
Beyond the arc, real-world integrity hinges on anticipating service conditions. Weld sequencing is strategically planned to counter residual stress, while nondestructive testing—ultrasonic or dye penetrant—catches subsurface flaws before they propagate. It’s this blend of metallurgical insight and practical foresight that separates a merely assembled frame from one engineered to endure decades of punishing use.
Assembly Sequence: Aligning Tolerances for Smooth Operation
Getting the assembly order right isn't just about following a list—it's about understanding how each part's tolerances stack up. When you sequence the steps thoughtfully, you can compensate for slight variations that might otherwise cause binding or excessive play. For instance, fitting a shaft into a housing before tightening bearing set screws lets you feel the alignment and adjust as needed, rather than forcing everything together and hoping for the best.
Tolerance alignment also means knowing which features are critical for function and which can be relaxed. By identifying the interfaces that dictate smooth motion, you can prioritize those fits during assembly. Sometimes a small shift in order, like preloading a spring or loosely fastening a cover until moving parts are cycled, dramatically improves how the mechanism feels. It's these subtle, experience-driven tweaks that turn a stiff or sloppy assembly into one that glides.
Final Testing: Stress Runs and Performance Calibration
Before any system goes live, we push it to its absolute limits. Stress runs aren’t just about cranking up the volume—they’re designed to uncover the subtle weak points that only emerge under sustained, chaotic demand. We simulate spikes in traffic, sudden data surges, and resource exhaustion scenarios, watching how every component holds together. It’s not about passing or failing; it’s about understanding the true breaking points and building in graceful degradation that keeps core operations ticking even when things get messy.
Performance calibration follows these stress sessions, turning raw observations into precise tuning. Bottlenecks get mapped, thread pools resized, and connection timeouts adjusted—not based on benchmarks alone, but on the actual shape of the workload the system will face. We often discover that the default configurations are overly cautious, leaving headroom on the table. By tightening those levers and retesting in iterative loops, we land on setups that feel snappy under normal load yet don’t crumble when the pressure spikes.
The final round always involves a reality check: real-world usage patterns tend to break assumptions made in isolation. Maybe your authentication service slows down unpredictably after 10,000 concurrent logins, or your caching layer starts purging early under mixed read/write traffic. That’s the stuff you only catch by blending stress runs with calibrated monitoring. Once everything stabilizes across these trial-by-fire scenarios, you’ve got more than a passing score—you’ve got a reliable feel for how the system will behave when it matters most.
FAQ
Start by clearly defining the shredder's intended throughput and material type, as these dictate the required power and cutter geometry. Then sketch a rough design, focusing on the rotor length, diameter, and bearing placement. Sourcing materials early, especially alloy steels for the shaft and blades, helps avoid delays.
Blades usually demand high wear resistance and toughness. Tool steels like D2 or A2 are popular because they hold an edge well under repeated impact. In some cases, holders use a milder steel like 4140 for better weldability, while the cutting edges are hardfaced with tungsten carbide for extreme durability.
The shaft must endure heavy bending and torsional loads without permanent deformation. Using a high-strength alloy such as 4340 or EN24, often heat-treated to achieve a hardness around 300–350 HB, prevents premature fatigue. A poorly chosen shaft can lead to misalignment, vibration, and early bearing failure.
For the frame, preheating thick steel plates before welding reduces residual stress and cracking. Techniques like submerged arc welding or MIG with proper filler metal produce deep, clean joints. Post-weld stress relieving in a furnace is also common to stabilize the structure and minimize distortion over time.
Balancing is critical—even a small imbalance can cause destructive vibration at operating speeds. We typically do a two-plane dynamic balance on the assembled rotor. Adding or removing weight at calculated positions on the end discs or shaft brings it within acceptable limits, often to G2.5 or better per ISO standards.
Heat treating is what transforms good steel into a long-lasting part. For blades, a proper hardening and tempering cycle can reach 58–62 HRC for edge retention. For shafts, quenching and tempering improves core strength while maintaining toughness. Without it, components wear quickly or fracture under shock loads.
A practical sequence is: mount the main bearings onto the shaft first, then lower the pre-balanced rotor assembly into the housing while aligning with the bolted bearing pedestals. Next, install the fixed knives with shims to set the cutting gap uniformly. Finally, bolt down the hydraulic cylinder and screen cradle, checking clearance at each step.
Before first run, verify all bolt torques, especially on cutter mounting and bearing housings. Measure the radial runout of the rotor at multiple points and confirm cutting gaps with feeler gauges. A dry rotation test by hand flags any binding. Then a no-load run at half speed for a few hours can reveal temperature rises or unusual noises.
Conclusion
Fabricating a robust single shaft shredder demands meticulous attention to the rotor's geometry and force distribution from the outset. The core design must evenly spread operational loads to prevent deformation and minimize stress concentrations during high-torque processing. Material selection becomes a critical trade-off between wear resistance and cost-effectiveness; the rotor and housing typically benefit from engineered alloy steels, while strategic use of hardened tool steels for high-wear zones prevents premature degradation without inflating the budget. Equally crucial is the forging and heat treatment of the cutting blades, where precise control over quenching and tempering achieves an optimal hardness profile—hard enough to shear through tough feedstocks, yet sufficiently ductile to resist chipping under sudden impacts.
Moving to structural fabrication, the machine's frame relies on carefully executed welding techniques to guarantee long-term rigidity and alignment. Distortion control during welding ensures that mounting surfaces remain true, a prerequisite for the subsequent assembly stage. During assembly, tight tolerance alignment between the rotor and counter-knives is essential; even minor deviations lead to uneven wear and power losses. The process culminates in a rigorous testing phase where stress runs under varying loads reveal any design flaws, followed by performance calibration to fine-tune speed, torque, and cutting clearance. This holistic integration of design, material science, and precise assembly yields a single shaft shredder built to withstand demanding industrial environments.
Contact Us
Contact Person: Leon
Email: [email protected]
Tel/WhatsApp: 8615385558866
Website: https://www.shred-waste.com