Multi Chamber Laundry Pods Exporter Guide to Reliable Sourcing
2026-11-02
Sourcing multi chamber laundry pods shouldn't feel like a gamble on chamber integrity or a guessing game with an exporter's real capabilities. This guide strips away the usual fluff to help you spot reliable partners before you commit to a container. We'll walk through the non-negotiables—dissolve rates, seam strength, and documentation—that separate durable pods from wash-day letdowns. You'll also see why importers keep circling back to LANJIEYA when they need a supplier that actually understands multi chamber production.
Spotting Red Flags in Multi-Chamber Pod Samples
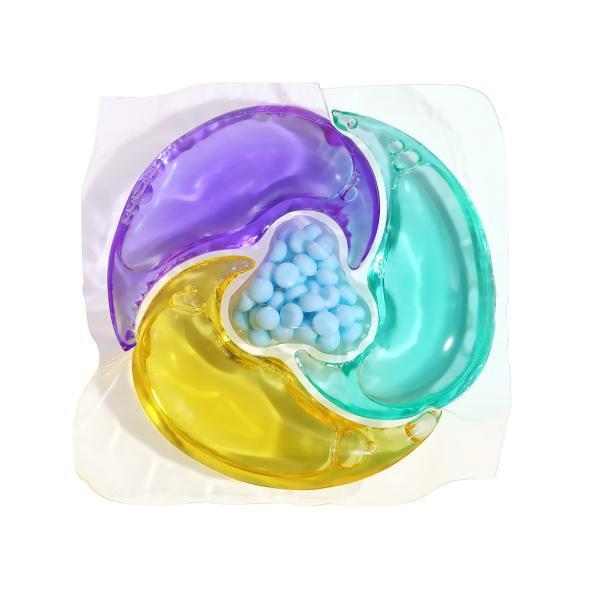
When evaluating multi-chamber pod samples, the first thing to look at is seal uniformity across each compartment. A weak or uneven seal often shows up as a faint gap, a wrinkled edge, or a slight lift where the film meets the pod rim. Run a fingertip along the perimeter—if you feel any tackiness or see micro-bubbles trapped in the laminate, that chamber may fail during shipping or use, causing cross-contamination between chambers.
Pay close attention to fill consistency between chambers. Even a slight variance in liquid level or powder density can indicate a dosing drift in the production line. Hold the pod against a backlight; shadows that don't align with the intended chamber walls suggest wall thinning or partial collapse. Additionally, any discoloration at the junction points—especially a hazy or milky band—often points to incompatible film layers reacting under heat sealing.
Finally, flex the pod gently between your fingers. A well-formed multi-chamber pod should feel uniformly resistant, with no crunching or sudden popping sounds from internal dividers. If you notice a chemical odor when opening the outer packaging, or if the individual chambers separate too easily with light pressure, treat those samples as suspect. Document each irregularity with photos and lot numbers before moving forward with any formulation or packaging decisions.
Reading a Supplier's Test Reports Like an Auditor
When you open a supplier's test report, don't just scan for the word "pass" and file it away. An auditor reads between the lines: check the date and lot number to confirm the report matches the exact shipment you received, not an older batch. Look for the test method and specification limits — a vague reference like "per internal standard" is a red flag unless you've already approved that standard. Pay attention to any omissions; if a critical parameter like moisture content or tensile strength is absent, ask why it wasn't tested. Real scrutiny means comparing the reported values against your own incoming inspection data. If the supplier's numbers are consistently tighter than yours, either their measuring equipment is better calibrated or someone is smoothing the edges. And never ignore the signature — an illegible scrawl or a generic "QA department" without a name tells you how seriously they take accountability.
A seasoned auditor treats a test report as a conversation starter, not a conclusion. Circle every value that sits close to the upper or lower limit, then request the raw data behind that single number. Many labs only report the average of three samples; ask for the individual readings to spot outliers that got averaged away. Check if the report references a recognized standard like ASTM or ISO — if it uses a company-specific method, compare it line by line against the industry norm. Also look for signs of hand-editing: a slightly different font on one line, a whited-out digit, or a unit that doesn't match the rest of the document. These small inconsistencies often indicate that someone altered the result after it left the testing equipment. A genuine report reads cold and technical; if it feels too polished or too brief, dig deeper.
Finally, read the report in context with the supplier's history. A new supplier who suddenly produces a flawless report for a complex product deserves more suspicion than praise. Pull their previous three shipments' reports and compare the test values — are they suspiciously identical? Real manufacturing has natural variation, so if the numbers never move, someone may be copy-pasting. Look at the test date versus the ship date: a report generated weeks before the goods were made is worthless. And check who performed the test — an in-house lab has an incentive to pass borderline material, while an independent third-party lab carries more weight. If the supplier refuses to share the underlying lab notebook or calibration records, treat that resistance as a failed test in itself. The goal isn't to catch every defect on paper, but to build a picture of whether the supplier's quality claims hold up under the same scrutiny you'd apply to your own production floor.
Why Chamber Separation Fails and How to Prevent It
Chamber separation often fails because the design assumes a perfect seal without accounting for thermal expansion, pressure spikes, or material fatigue. In practice, gaskets creep, bolts loosen unevenly, and micro-gaps open between mating surfaces. Once a leak path forms, it widens under cyclic loading, and the isolation that seemed solid on paper becomes a source of cross-contamination or pressure loss. Fixing this after the fact is expensive, so the real question is how to build in tolerance from the start.
Prevention starts with acknowledging that separation is a system problem, not a single-component issue. Instead of relying on one robust barrier, use a layered approach: select materials with similar thermal expansion rates, machine flanges to a controlled flatness, and apply a preload that stays within the elastic range of the fasteners. Regular torque audits catch early loosening before it becomes a leak, and adding a soft metallic or graphite gasket can compensate for minor surface irregularities that would otherwise compromise the seal.
Another common failure driver is misalignment during assembly. If the chamber halves are forced together under uneven stress, the seal may hold initially but fail prematurely once the system reaches operating temperature. A practical method is to use alignment pins or dowels during fit-up, and to tighten bolts in a star pattern with incremental passes. Coupling this with a short pressure-hold test before full operation reveals weak spots while they are still cheap to correct. Ultimately, preventing chamber separation is less about exotic materials and more about disciplined assembly and maintenance routines that respect the actual conditions the chamber will face.
Negotiating Bulk Orders Without Sacrificing Fill Quality
Bulk order negotiations often zero in on price per unit, and that narrow focus can quietly erode fill quality. When volume spikes, the temptation is to relax inspection frequency, accept looser packaging specs, or let line-item accuracy slide in exchange for a few cents off. Instead, treat fill quality as a measurable part of the deal from day one. Define exactly what acceptable means—order accuracy rates, damage thresholds, fill rate percentages—and pin those numbers into the agreement alongside the pricing table. This keeps the conversation balanced and prevents later claims that “higher volume naturally means more errors.”
A practical approach is to build quality commitments into the quote itself. Ask the supplier or fulfillment partner to include a short quality assurance plan with their bulk pricing, covering how they’ll scale labor, equipment, and checks without cutting corners. You can also agree on a phased ramp-up: the first few thousand units go through full inspections, and only if defect rates stay under a set limit do you release the rest of the order at the negotiated rate. This gives both sides a clear incentive—the seller keeps the large order, and you avoid accepting a warehouse full of subpar fills.
Finally, use negotiation leverage on variables other than fill quality. If the supplier pushes back on your quality metrics, offer flexibility on payment terms, delivery windows, or packaging branding in return for holding the line on fill accuracy and damage rates. This signals that you’re not just driving down cost but protecting the end customer’s experience. Keep the tone collaborative: “We want the volume to work for both of us, and here are the three quality benchmarks we can’t compromise on.” That framing often unlocks better concessions than a purely transactional back-and-forth.
The Hidden Costs of Thin Film and Weak Seals
Thin film might look like a bargain on the spec sheet, but the real expenses show up long after installation. Films that tear during routine handling, degrade under UV exposure, or lose their barrier properties within a few seasons force repeated replacements. Each replacement isn't just a material cost—it's downtime, labor hours, and often damaged goods that had been relying on that film for protection.
Weak seals are even more insidious because the failure rarely announces itself. A seal that seems tight on day one can creep open under temperature swings, vibration, or simple pressure from stored contents. By the time the leak is noticed, moisture or contaminants have already done their work. The result is silent inventory loss, warranty claims, and a creeping reputation problem that no amount of after-sales support can fully undo.
The hidden costs compound when you factor in rework and emergency replacements. A facility that tries to save a few cents per unit on film or sealing often ends up paying for expedited shipping, overtime labor, and scrapped batches. Over a year, these unplanned expenses dwarf any upfront savings—and they're rarely tracked under a single line item, so the pattern repeats.
Keeping a Shipment Intact Through Heat, Cold, and Customs
Keeping a shipment intact across temperature swings and border checkpoints rarely hinges on a single safeguard. For heat and cold, the real difference comes from matching insulation and refrigerants to the exact route duration, not just the product category. A pallet of enzyme reagents moving through Dubai in August might need vacuum-insulated panels plus pre-conditioned gel packs, while frozen seafood crossing Canada in February is often better served by a thick polyurethane liner and dry ice calculated for an extra 36 hours of dwell time. Small details like pre-cooling the container, placing temperature loggers next to the goods rather than on the wall, and using phase-change materials with the right melting point prevent most thermal failures before the truck ever moves.
Customs is where otherwise stable cargo gets compromised. The fastest way through is to file complete, consistent paperwork before departure: commercial invoice, packing list, and any permits or certificates should describe the goods in the same language and HS code classification that the destination country expects. A customs broker who regularly handles temperature-sensitive freight can flag issues like wooden pallet treatment requirements or restricted biologics early, so your shipment is not held in an unshaded inspection bay at noon. When delays do happen, having a contingency plan—such as a pre-arranged local cold storage partner or a courier authorized to plug in active containers—often determines whether the cargo arrives intact or becomes a costly write-off.
FAQ
Look beyond the website. Request a copy of their export license, audit reports from a recognized third party, and samples from an actual production batch rather than a lab batch. Confirm they own or directly control the blending and sealing lines—many trading companies claim factory status but cannot trace a batch to a specific production date.
Multi chamber pods require precise separation of incompatible ingredients until the wash cycle begins. That means the water-soluble film must have consistent dissolution timing across each chamber, and the sealing pressure must be uniform. Ask the exporter for film compatibility data and burst strength tests for every color-coded chamber, not just a generic spec sheet.
For Europe, look for REACH compliance and a safety data sheet that matches the exact fragrance and enzyme package. For North America, expect EPA Safer Choice or equivalent, plus child-resistant packaging certification. If the exporter cannot show a recent certificate of analysis for the PVA film lot, keep looking.
Many factories quote 30,000 to 50,000 units as a soft minimum, but serious custom formulations often start around 100,000 units. Smaller orders usually mean you are buying a stock formulation with a label change, not true private label chemistry. Negotiate for a trial run of 5,000 to 10,000 units before committing to a container load.
Request a live video walkthrough of the production floor with the current date visible, ask to see the retained samples from the last three export shipments, and pay for a pre-shipment inspection by an independent lab that tests dissolution rate, pH, and sealing integrity. A reliable exporter will agree to these terms without charging an extra inspection fee upfront.
The PVA film softens in high humidity and becomes brittle in very dry conditions, so the container must be moisture-controlled. Multi chamber pods also have a higher risk of chamber-to-chamber leakage if pallets are stacked too high. Specify shrink-wrapped, double-wall cartons and require a temperature data logger inside at least one carton per pallet.
Watch for vague answers about the source of the film, reluctance to provide the enzyme supplier name, or a sudden price drop after you question the formulation. Also be wary of exporters who offer extremely fast delivery on custom colors—proper film testing takes at least two to three weeks. If they skip that, you will likely see leaking pods in transit.
Split the order into two phases: a paid pilot batch of 10,000 to 20,000 pods for sink, washing machine, and accelerated stability testing, followed by the main production run only after approval. Keep 10% of the payment until an independent inspection confirms the sealed load. This gives you leverage if the film quality or chamber separation fails.
Conclusion
Sourcing multi-chamber laundry pods from overseas demands more than a competitive quote; it requires a disciplined eye for sample flaws that often predict batch-level disasters. Start by tearing into sample pods under bright light: uneven chamber fill, sticky seams, or a transparent film that feels brittle to the touch are early warnings no spec sheet will confess. When a supplier hands you test reports, treat them as a puzzle rather than a verdict. Compare stated dissolution times against your own sink test, check the age of the lab data, and confirm the report actually matches the pod variant you were sent—mismatched lot codes are a classic trick. Chamber separation fails not from a single bad batch but from rushed lamination and poor humidity control on the line. The preventive fix is boring but non-negotiable: demand footage of the sealing station, ask for film tensile strength in both machine and cross directions, and set a minimum burst threshold for each chamber wall.
Bulk order negotiations usually collapse around price per pod, but the real leverage lies in fill quality guarantees. A factory can shave a gram of detergent from every chamber and still call it "spec-compliant"—until your customers complain about weak stains. Insist on a written tolerance of ±2% fill weight and a retained-sample clause that lets you audit random cartons after production. Thin film and weak seals feel cheap at the quote stage but surface later as burst pods, leaking gel, and a flood of return requests. Factor in the hidden cost of re-inspection, repackaging, and damaged retailer relationships, and the higher upfront film cost almost always wins. Finally, plan for the journey: multi-chamber pods hate extreme heat, which softens seals, and freezing cold, which makes film shatter. Require insulated container liners for summer shipments, avoid unheated warehouses in winter, and keep your customs paperwork so precise that a two-day border delay never turns into a sweating, leaking pallet. Reliability is not found in a single perfect sample; it is built in the boring checks you repeat every order.
Contact Us
Contact Person: Zhao Yanlong
Email: [email protected]
Tel/WhatsApp: 8615832007309
Website: https://www.gzlanjieya.com