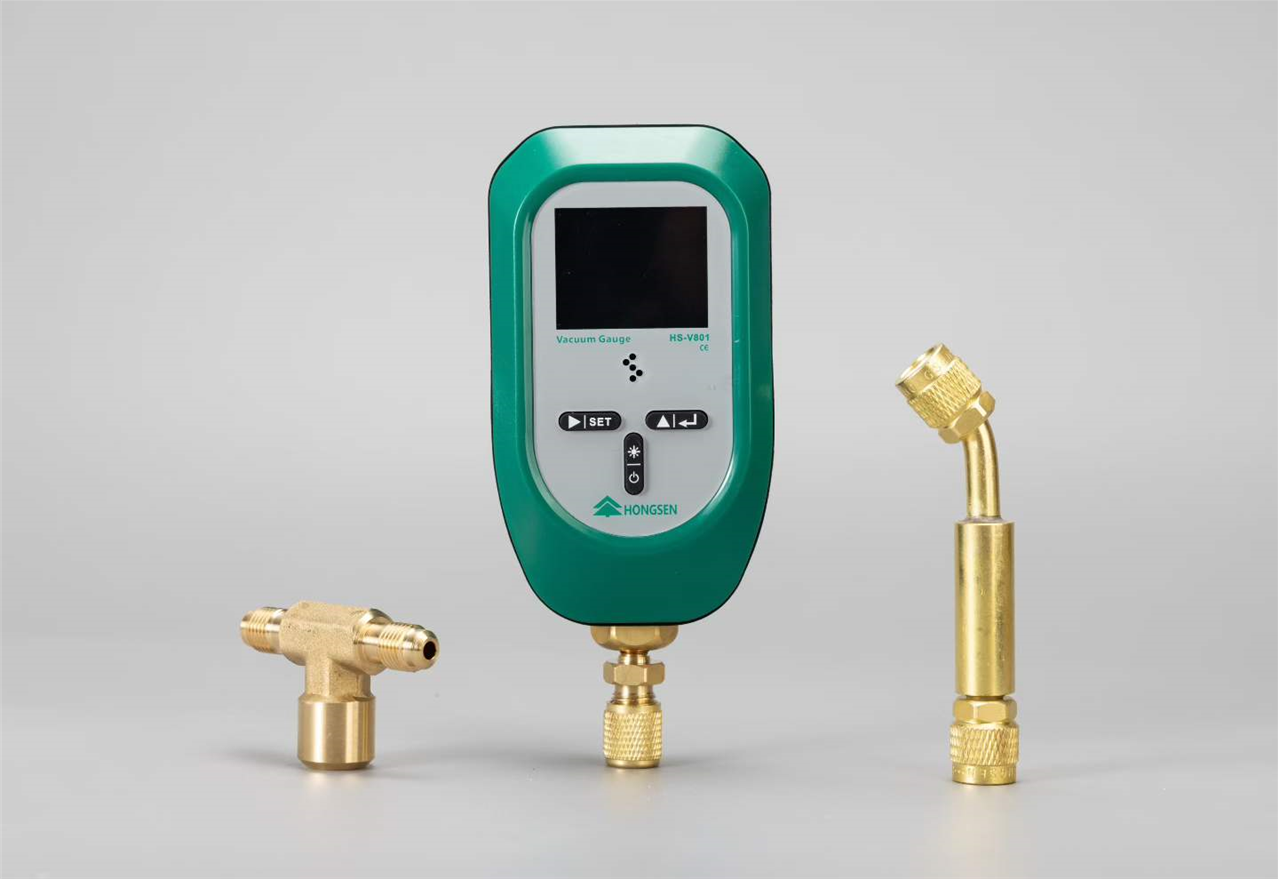
Digital Vacuum Gauge Manufacturer Guide for Reliable Vacuum Measurement
2026-11-16
You don't need another brochure promising 'high accuracy.' You need to know why one digital vacuum gauge keeps delivering stable readings at 10^-3 Torr while another drifts after a week. This guide is built for that question—drawing on manufacturing insights from HONGSEN, where vacuum measurement isn't a sideline. We'll cover the practical details that decide whether your readings hold up when it counts.
Why Sensor Type Matters More Than Brand Name
It’s easy to assume that a well-known logo guarantees better tracking, but that’s rarely how the hardware actually works. Most brands don’t manufacture their own sensors; they buy them from a handful of specialized suppliers. Two mice from completely different companies can share the exact same internal sensor, while two models from the same brand might use vastly different components. So the name printed on the shell tells you almost nothing about how the cursor will behave.
The sensor type is what dictates real-world performance: how fast you can flick without losing control, how smoothly it tracks on unusual surfaces, and whether the lift-off distance feels predictable. Optical and laser sensors, for example, have distinct strengths and weaknesses that no amount of brand engineering can erase. A high-quality optical sensor will beat a mediocre laser one every time, regardless of the logo next to it.
If you’re comparing options, ignore the marketing fluff and look for concrete sensor specs like maximum tracking speed, acceleration, and resolution range. A budget mouse with a proven top-tier sensor will almost always outperform a premium-brand model that hides a generic sensor behind fancy RGB lighting. Spend your money on the part that actually does the work.
Decoding Accuracy Specs Without Falling for Marketing Claims
Manufacturers love to throw around numbers like ±0.01% accuracy, but those figures often come from idealized lab conditions that have little to do with real-world use. A sensor might hit that spec on a test bench, yet drift or behave differently once temperature shifts, humidity creeps in, or the device ages. The first step is to recognize that a single spec without context is little more than a sales pitch.
When comparing products, dig into the fine print. Look for the full test conditions: over what temperature range, at what supply voltage, and for how long after calibration? A spec that says "±0.1% typical" is far weaker than "±0.05% maximum over -40°C to 85°C." Also pay attention to units and reference points—some vendors quote accuracy as a percentage of reading, others as a percentage of full scale, and the difference can be enormous at low signal levels.
Finally, lean on independent verification whenever possible. User communities, tear-down reviews, and long-term reliability reports often reveal whether a device actually holds its claimed precision outside the marketing brochure. If a vendor can't provide detailed test data or dodges questions about measurement uncertainty, that's a sign to look elsewhere. Trust specs that are boring, specific, and backed by evidence—not the flashy headline numbers.
Installation Mistakes That Quietly Ruin Vacuum Readings
Mounting the gauge directly on a pump inlet is a classic error. The pressure you see there reflects the pump's throat, not the chamber volume where your process actually happens. Gas flow is still churning through the line, so the reading can be off by an order of magnitude until things settle down.
Tiny leaks around compression fittings or KF flanges won't stop a system from reaching rough vacuum, but they can keep a chamber stuck in the low 10^-5 torr range while you chase ghosts in the pump or the sensor. A quick shot of helium around every joint tells you more than another hour of leak checking the pump itself.
Putting a hot cathode gauge in a spot that sees sudden air inrushes during venting will kill the filament fast. Once that filament is poisoned, the readings drift silently upward, and you end up trusting a number that has nothing to do with actual pressure. Even a small vibration from a nearby roughing pump can cause a cold cathode gauge to spark and give spurious readings.
Calibration Schedules That Fit Real Production Demands
Calibration schedules usually get treated like a fixed calendar event, but real production rarely works that way. A line running three shifts with abrasive materials won't hold tolerance the same way as a lightly used bench-top unit. Instead of forcing every instrument into the same quarterly box, successful teams map calibration triggers to actual wear patterns, usage hours, and drift history. That might mean a torque wrench on a critical joint gets checked every 500 cycles while a temperature probe in a stable cleanroom goes nine months without issue. The goal isn't more frequent calibration—it's calibration at the moment it actually matters.
Production demands shift weekly: a new product ramp, a sudden batch of high-precision parts, or a borrowed machine from another line. Rigid schedules break under that pressure. One approach is to build a tiered system where instruments are grouped by risk and consequence. Critical gauges that feed SPC data or release product get short, condition-based intervals. Support equipment with wide tolerance bands can run on a longer cycle with a simple functional check in between. This keeps the calibration lab focused on what could actually stop a line or ship a bad part, rather than chasing paperwork for tools that haven't drifted in years.
The practical side is just as important. A schedule that looks perfect on a spreadsheet fails if it takes a machine offline at peak demand. Many plants now stagger calibration windows around planned maintenance, tooling changes, or low-volume periods. Some use a small buffer of pre-calibrated backup instruments so a critical gauge can be swapped in minutes instead of waiting for the lab. Others extend intervals only after reviewing six months of stable calibration history. The result is a schedule that production actually follows—not one that gets quietly ignored when the order book fills up.
When to Repair, Replace, or Upgrade Your Vacuum Gauge
A vacuum gauge that starts drifting, responds sluggishly, or gives inconsistent readings doesn't always mean it's time to throw money at a new unit. For high-end capacitance manometers or ionization gauges, a straightforward repair—like replacing a contaminated sensor, cleaning internal baffles, or recalibrating the electronics—often restores performance at a fraction of the cost. Pull the service manual and check the error history first. If the failure is isolated to a known wear component and the gauge body is still sound, repairing makes far more sense than replacing.
The case for replacement becomes clear when repair quotes creep past half the price of a new gauge, especially if the unit is older and parts are getting scarce. Age also matters: a ten-year-old Pirani gauge with a worn filament and outdated firmware may keep failing every few months, costing you more in downtime than a modern equivalent. Before you decide, compare the cost of a repair kit plus labor against a current model that likely uses better materials and has a longer warranty. If the math doesn't favor repair, replace without guilt.
Upgrading is a different conversation altogether. When your process moves toward lower base pressures, harsher chemistries, or stricter repeatability requirements, an older gauge may simply lack the range or accuracy you now need. For instance, swapping a thermal conductivity gauge for a heated capacitance diaphragm gauge can deliver better resolution in the 0.1–100 Torr window, while a cold cathode unit might eliminate filament burnout issues in reactive gas lines. Look at your recent calibration drift, the time spent chasing ghost leaks, and whether a newer sensor technology would let you automate or log data more easily. If any of those pain points show up weekly, an upgrade pays for itself sooner than expected.
Choosing a Manufacturer That Understands Your Process, Not Just Your Purchase Order
A manufacturer that only sees your purchase order will treat every job as a one-off transaction. They might hit the specs on paper, but they miss the context—how this part fits into your assembly, what stresses it will face in the field, or why you chose a particular material. When a manufacturer takes time to understand your actual production process, they can point out that a slight change in radius would prevent cracking during installation, or that a different surface finish would speed up your downstream coating step. That kind of insight doesn't come from reading a drawing; it comes from walking your floor and asking why you do things a certain way.
This deeper involvement changes the nature of problem-solving. Instead of reacting to quality issues after parts arrive, you get a partner who flags risks before tooling is cut. For example, if your process involves a secondary heat treatment, a manufacturer who knows that can adjust initial dimensions to compensate for expected distortion, saving you from a costly batch of out-of-tolerance parts. They become an extension of your engineering team, not just a vendor waiting for the next RFQ.
Over time, this relationship compounds. You stop re-explaining your requirements with every order, and the manufacturer starts anticipating your needs based on past projects and evolving product lines. The result is fewer delays, less rework, and a supply chain that feels less like a series of transactions and more like a shared effort to build something reliable. That's the difference between a vendor who ships boxes and a partner who helps you ship better products.
FAQ
Pay close attention to how they handle sensor protection and long-term drift. Many suppliers list impressive accuracy specs, but real-world reliability often comes down to whether the gauge can tolerate process contamination without frequent recalibration. Ask about their vacuum sensor technology, warranty terms, and what kind of service turnaround they actually deliver.
The obvious difference is the numeric readout, but the practical benefit is faster interpretation and fewer reading errors. Digital gauges also tend to include data logging, set point relays, and communication options that simplify process control. You give up the sweeping needle visual, but most technicians adapt quickly because the numbers are unambiguous.
For rough vacuum, a Pirani or thermal conductivity gauge is usually the sensible starting point. They are rugged and inexpensive. If your process involves reactive gases or frequent pressure cycling, make sure the manufacturer uses a corrosion-resistant filament or offers a protected sensor version. Otherwise accuracy can degrade after just a few weeks.
Drift typically comes from sensor contamination, temperature swings, or low-quality analog front-end components. A good manufacturer will specify drift per year under clean conditions and provide an in-situ calibration function. If a supplier cannot give you a drift specification, treat that as a warning sign rather than a minor omission.
It depends on your internal metrology capability and the gauge design. Some gauges support one-point or two-point field calibration against a reference standard, which is fine for trending. For ISO-certified processes or when the gauge is used as a master reference, factory calibration with traceable documentation is worth the downtime and shipping cost.
The most common mistake is placing the gauge too far from the chamber or in a line with poor conductance. Another frequent issue is mounting the sensor where condensable vapors can pool. Use short, wide connections, keep the gauge at the same temperature as the process, and avoid dead legs. Even a top-tier gauge will report wrong values if the installation geometry is poor.
For fast-cycling systems, response time matters more than absolute accuracy. A gauge that updates once per second may be fine for a furnace, but a load lock or leak test rig needs millisecond-level response. Ask for the time constant under your actual pressure range, not just the sensor response in clean air, because the two numbers can be very different.
Beyond a warranty, look for accessible application engineers, repair services that quote turnaround in days not months, and a clear calibration history. Some manufacturers will loan you a replacement gauge while yours is being serviced. That kind of support often matters more than a 0.1% accuracy difference on a datasheet.
Conclusion
Reliable vacuum measurement starts with choosing the right sensor for your pressure range, not chasing a familiar brand name. A Pirani gauge works well in rough vacuum but drifts in high vacuum, while a capacitance diaphragm gauge holds calibration better in harsh processes. Accuracy specs are equally tricky: “0.5% of full scale” can mean a huge error at low readings, so you need to check whether the figure is based on reading or span. Beyond the sensor, installation details quietly decide data quality. A gauge mounted too close to a pump inlet or in a dead-leg pipe will read pressure that doesn't exist in the chamber, and small leaks or contamination film on the sensor can shift readings without any warning.
Calibration should follow actual usage intensity, not a fixed calendar date—a gauge in a clean coating line may need checking every three months, while one in a dusty packaging line might need monthly verification. Watch for slow zero drift or noisy output as early signs that repair or replacement is cheaper than a bad batch. When upgrading, don't just compare datasheets; find a manufacturer that asks about your process temperature, gas composition, and cycle timing. A supplier who understands that a freeze dryer behaves differently from an electron-beam welder will give you better mounting advice, recalibration intervals, and failure warnings. That kind of partnership, not a generic purchase order, is what keeps your vacuum measurements trustworthy year after year.
Contact Us
Contact Person: KOPASS HO
Email: [email protected]
Tel/WhatsApp: 8613606566112
Website: https://www.hongsenref.com/