Custom Vapor Barrier OEM Solutions for Superior Moisture Control
2026-08-03
When it comes to protecting your building from the silent threat of moisture, off-the-shelf solutions often fall short. That’s where custom OEM vapor barriers make a critical difference—and Jinbo is redefining what's possible. With tailored engineering and advanced materials, Jinbo’s OEM solutions deliver superior moisture control that adapts precisely to your project’s demands. In this post, we’ll peel back the layers on how custom vapor barriers can save you from costly damage, boost energy efficiency, and why a one-size-fits-all approach just doesn’t cut it. Get ready to rethink moisture management.
Crafting Tailored Moisture Defense for Unique Project Demands
Every project carries its own fingerprint—environmental quirks, material preferences, and long-term performance expectations that off-the-shelf solutions rarely satisfy. Instead of bending your requirements to fit a pre-packed product, we reverse the process: assessing the specific moisture load, substrate sensitivity, and lifecycle demands of your structure to formulate a barrier that shields without compromise. This approach sidesteps the fatigue of generic membranes that fail early or complicate installation, delivering protection that feels almost intuitive to the build.
Our work leans on a deep materials palette—polyurethane hybrids, cementitious coatings, and bitumen-free options among others—each selected and stacked where it makes the most sense. A coastal substation’s salt-laced air, for instance, demands a vastly different tactic than a heritage basement’s lime masonry. By tuning flexibility, adhesion, and vapor permeability at the recipe level, we create membranes that move with the building and lock out water without trapping moisture inside, preserving both structure and character.
The real difference emerges during application. We align curing times, surface prep, and joint detailing with your site’s rhythm, removing the disconnect between lab specs and field reality. On one recent art storage facility, this meant laying down a cold-applied system that emitted zero VOCs during sensitive collections handling—no heat, no odor, no margin for error. This level of specificity transforms moisture defense from a checklist item into a crafted layer of certainty that lasts decades, not seasons.
Precision-Engineered Materials for Lasting Protection
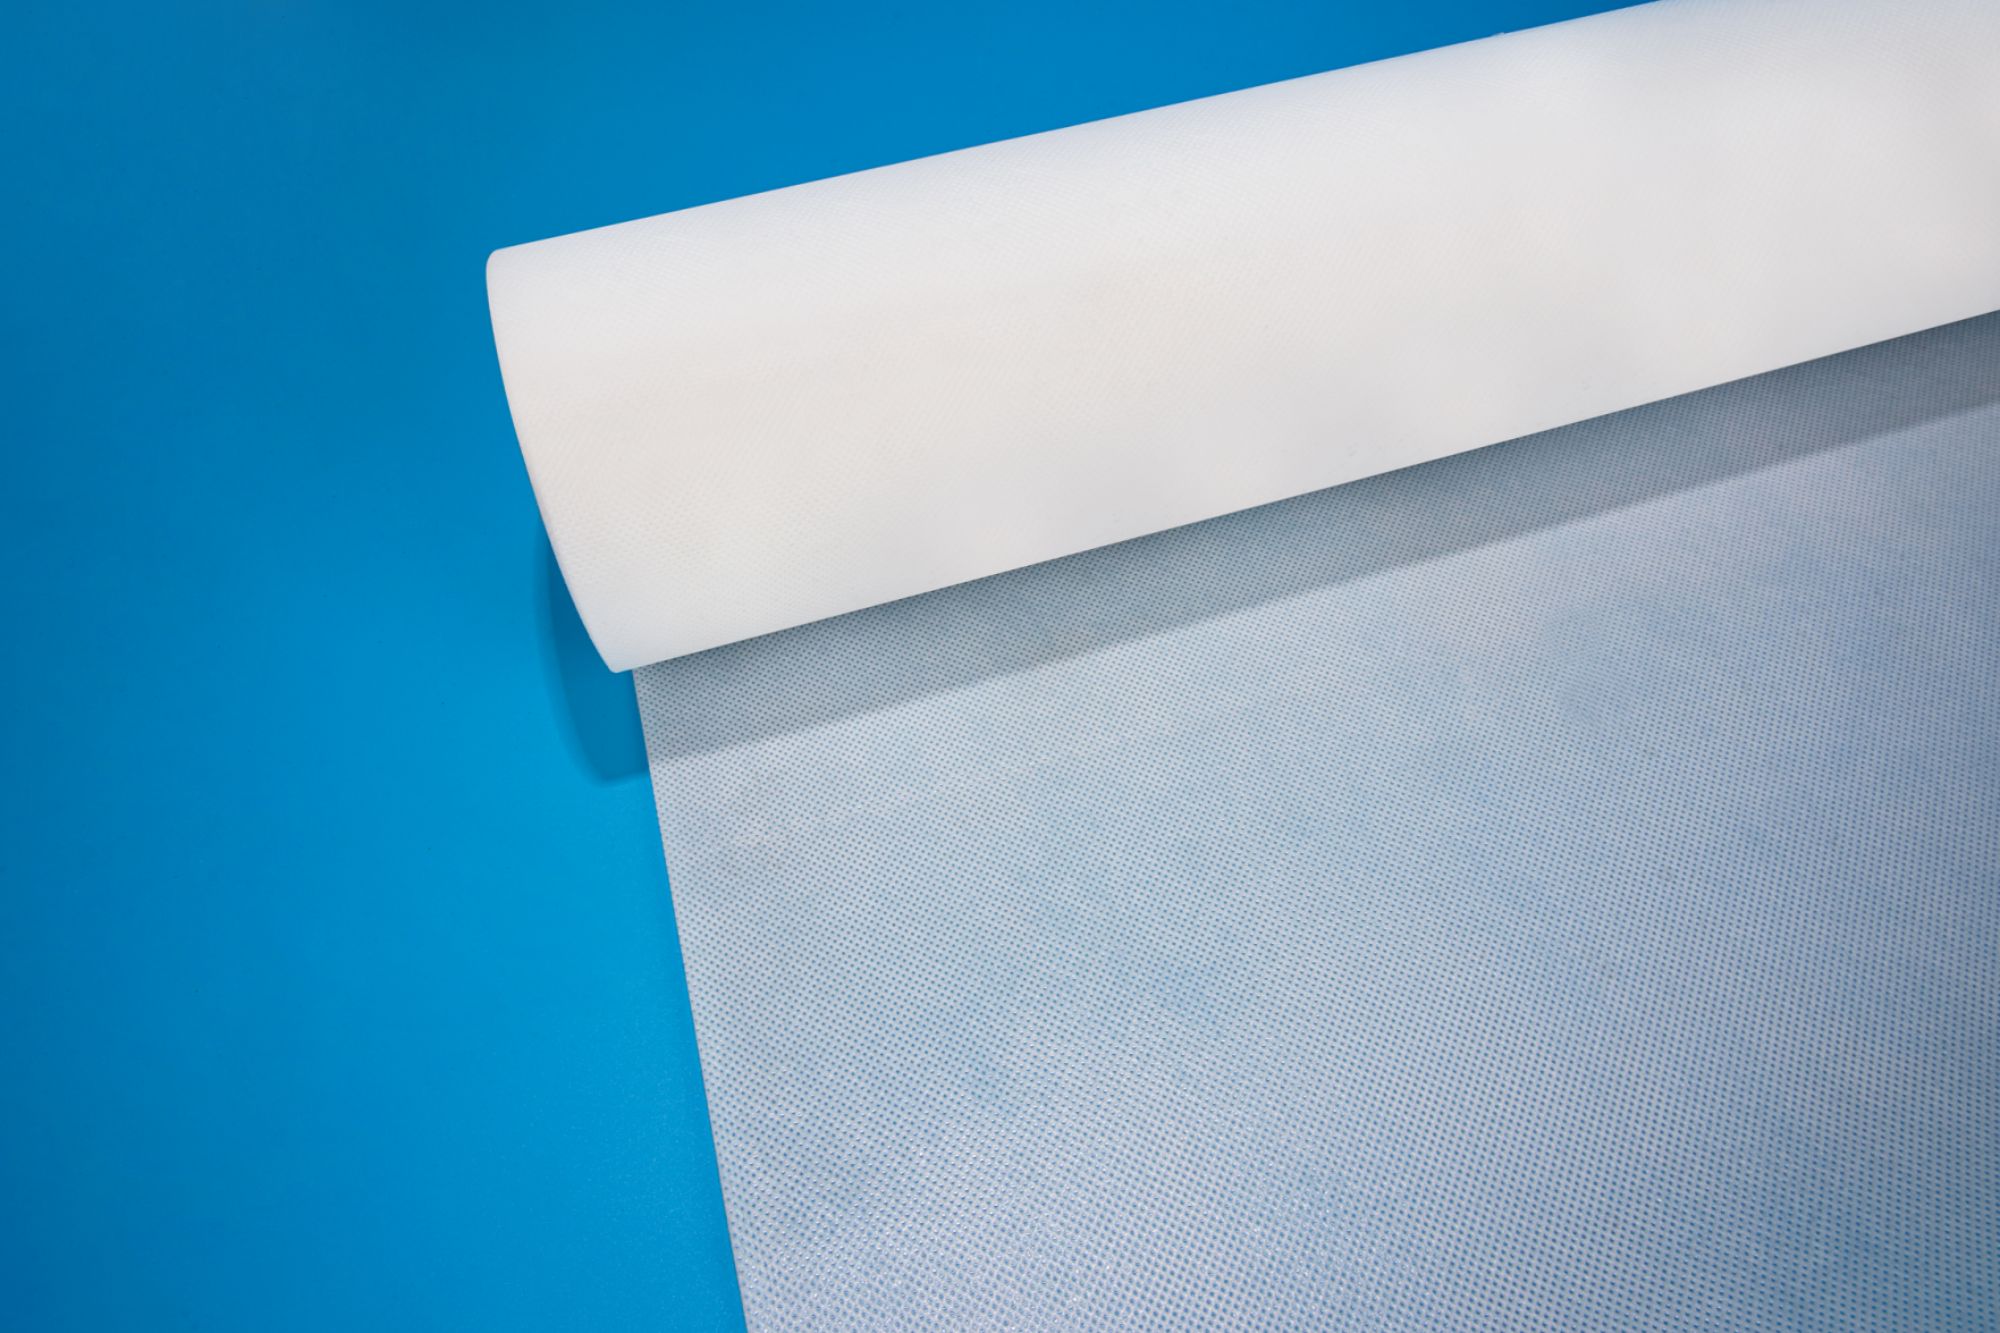
The protective qualities of a material often hinge on how precisely its structure aligns with the demands of its environment. It’s not just about adding thickness or using a stronger base substance—it’s about tailoring the material at a microscopic level. By controlling grain boundaries, phase distribution, and surface chemistry, engineers create barriers that actively resist degradation. These materials don’t just sit there; they interact with corrosive agents, heat, or mechanical stress in ways that neutralize threats before they can take hold. The result is a component that behaves more like a self-regulating system than a passive shield.
In practice, this means moving beyond generic alloys and coatings to solutions designed for a specific job. Take a high-temperature turbine blade, for instance. The material isn’t simply heat-resistant—it’s engineered to form a stable oxide layer that regenerates as it’s worn away, constantly renewing the protective surface. Or consider a seal in a chemical processing plant, where the elastomer is compounded not just to withstand solvents but to swell just enough to tighten the seal without losing integrity. Each formulation is a deliberate balancing act, tested against the exact conditions it will face rather than a one-size-fits-all specification.
Durability doesn’t come from overbuilding; it comes from this level of precision. When materials are tuned to their purpose, they last longer without excess weight or cost, and they often require less maintenance because the protection is inherent rather than applied. This approach shifts the focus from treating symptoms—like repairing corrosion damage—to preventing it from the start. In long-term installations, that not only extends service life but also reduces downtime and the environmental toll of replacements, making precision-engineered materials a quiet yet powerful force behind reliable infrastructure.
Seamless Integration with Your Existing Manufacturing Processes
Bringing new equipment into a production line often feels like forcing a square peg into a round hole. Our team designs every system with your current setup in mind, using modular interfaces and communication protocols that talk directly to your PLCs, SCADA networks, and MES platforms. No need to rip out what already works—our engineers map data paths and control logic so the handshake between old and new is practically invisible.
The real test of integration comes during changeovers and maintenance. We embed diagnostics that mirror your existing alarm hierarchies and troubleshooting workflows. Operators won’t have to learn a separate fault-code language; the system flags issues exactly where they’re used to looking. Maintenance crews can swap modules without reconfiguring upstream or downstream stations, minimizing line stoppages that erode OEE.
Beyond the physical layer, we align digital threads so your traceability and reporting remain unbroken. Batch records, serialization data, and quality metrics merge into your central archive without manual transcription. Whether you run a legacy ERP or a cloud-native MES, the integration preserves data continuity—no synchronization gaps, no dropped handshakes, just one cohesive manufacturing loop.
Advanced Barrier Technology That Adapts to Extreme Environments
Barriers that hold up under severe conditions often rely on materials and design principles that go beyond static resistance. The key lies in dynamic adaptability—structures that can alter their physical or chemical properties in real time as external stressors intensify. This might involve polymer matrices that become more cross-linked when exposed to high heat, or surface coatings that reorganize at a molecular level to reject ice, salt, or corrosive agents. Rather than simply withstanding an assault, these systems respond like living tissue, channeling energy and redistributing stress to prevent catastrophic failure.
One approach that has shown remarkable promise is the integration of shear-thickening fluids into composite layers. In ordinary conditions, the material remains flexible and lightweight, but upon sudden impact or high strain rates, it stiffens instantly. This transition is not triggered by any external controller; it's an inherent material response. Combined with microencapsulated healing agents that release when cracks begin to propagate, the barrier effectively self-diagnoses and repairs damage that would normally require manual intervention. Such technologies have already found their way into protective gear for aerospace components and deep-sea installations where maintenance is nearly impossible.
Beyond passive toughness, these advanced barriers can incorporate sensing elements that feed data to monitoring systems, enabling predictive adjustments before conditions turn critical. For instance, embedded fiber optics can detect temperature gradients and trigger phase-change materials to redistribute thermal loads. This creates a barrier that isn't just a wall but an active participant in environmental management. The result is a system that extends service life, reduces downtime, and often eliminates the need for secondary protective measures. In extreme environments—from arctic platforms to molten-salt reactors—such adaptive barriers are moving from experimental concepts to operational necessities.
Elevating Product Longevity Through Strategic Vapor Management
Moisture and vapor often silently chip away at a product’s lifespan, leading to corrosion, warping, or electrical failures that surface only after sustained use. By controlling how vapor moves within and around a device, manufacturers can prevent these slow, cumulative damages. Strategic placement of breathable membranes or desiccants, for instance, redirects humidity away from sensitive components, ensuring that internal environments stay stable even when external conditions fluctuate. This isn’t about sealing everything off—complete isolation can create pressure differentials or trap condensed moisture—but about giving vapor a controlled path that respects the product’s architecture.
The real advantage emerges when vapor management is treated as a dynamic system rather than a static barrier. Materials that adapt to humidity levels, such as polymer blends that expand to block moisture ingress during high-humidity exposure, can significantly extend operational life without adding bulk. In electronics, this might mean the difference between a device that survives a humid warehouse for years and one that starts corroding within months. Similarly, in packaging, using vapor-phase inhibitors that release protective molecules gradually can shield metal parts during long-term storage. The focus shifts from merely delaying degradation to actively preserving integrity, turning vapor from a threat into a manageable factor.
Designing for longevity through vapor control also changes how we think about product maintenance and warranty. Instead of accepting vapor-related failures as inevitable, engineers can embed indicators that signal when adsorbent materials are saturated, prompting timely replacement. This proactive approach not only reduces waste but also builds trust with users who see products remaining reliable far beyond typical expectations. Whether in automotive sensors, industrial machinery, or consumer gadgets, a well-executed vapor strategy quietly underlies extended performance, proving that the invisible details often matter most.
Partnering from Concept to Completion for Reliable OEM Delivery
From the very first sketch, we embed our engineering know-how right beside your ideas. Instead of a handoff, it’s a true exchange—your requirements evolve with our production insights, catching potential snags long before tooling begins. This joint approach turns ambiguity into a clear roadmap, so what lands on the manufacturing floor already carries the stamp of mutual confidence.
As milestones come and go, the rhythm of our collaboration stays constant. Prototypes are not just review items; they’re open conversations that tighten tolerances and squeeze out inefficiencies without flame. By the time the final units roll off the line, every process step has been stress-tested through this shared lens. The outcome is more than a delivered OEM order—it’s a product that mirrors the trust built along the way.
FAQ
Custom vapor barrier OEM solutions are tailored moisture control products manufactured by one company under another brand's name. These solutions are designed to meet specific application requirements, offering superior protection against moisture ingress in construction, packaging, and industrial settings.
They use high-performance materials like reinforced polyethylene or aluminum laminates, combined with advanced sealing technologies. Customization can include multi-layer structures and desiccant additives to actively manage humidity, ensuring long-term effectiveness even in extreme conditions.
Absolutely. Thickness, puncture resistance, tensile strength, and flexibility can all be customized. We work with you to specify the exact mechanical and permeability characteristics needed for your project.
Construction (under-slab and crawl space applications), electronics packaging, military storage, and food preservation. Any sector where precise moisture control is critical can benefit from a customized solution.
It starts with a detailed consultation to define requirements, followed by material selection and prototype development. After rigorous testing and client approval, we handle full-scale production, quality assurance, and logistics, delivering ready-to-brand products.
Yes, we understand the need for testing. We offer flexible MOQs, starting with small batches for prototyping and market trials, before scaling up to larger production runs.
Conclusion
Custom vapor barrier OEM solutions deliver meticulously designed moisture defense systems that align precisely with the unique requirements of each project. Materials are selected and engineered at a granular level, ensuring that the barrier not only blocks moisture effectively but also resists long-term degradation. Rather than relying on off-the-shelf products, the focus remains on developing a barrier that matches the substrate, environmental exposure, and expected service life of the application. This approach eliminates guesswork and reduces the risk of premature failure, whether the need is for flexible packaging, construction underlayments, or industrial containment. Advanced polymer chemistries and multi-layer constructions are refined to create barriers that maintain their integrity even under fluctuating humidity and temperature cycles.
These solutions integrate directly into existing production workflows, avoiding costly retooling or process overhauls. Through close collaboration from initial concept through final delivery, every stage is streamlined to ensure consistent quality and on-time supply. The technology adapts to extreme environments, from sub-zero cold storage to high-heat processing lines, preserving both product integrity and operational efficiency. By managing vapor transmission strategically, the lifespan of end products is extended, reducing waste and warranty claims. This partnership model—focused on engineering, prototyping, and scaled manufacturing—ensures that the vapor barrier performs reliably across its intended use, turning a potential point of failure into a competitive advantage.
Contact Us
Contact Person: Miranda
Email: [email protected]
Tel/WhatsApp: +8615231299719
Website: https://www.ihousewrap.com/